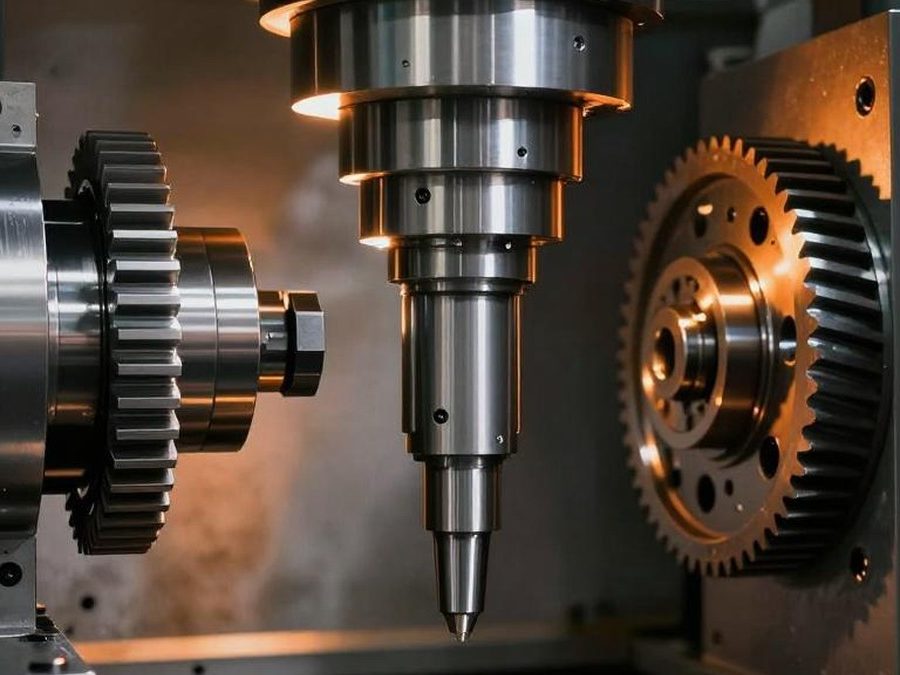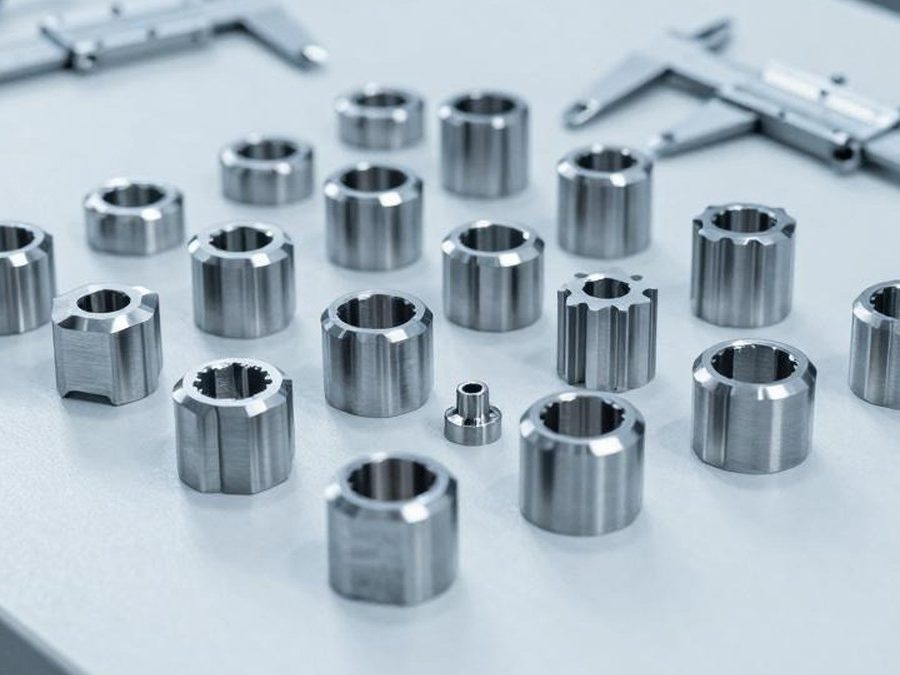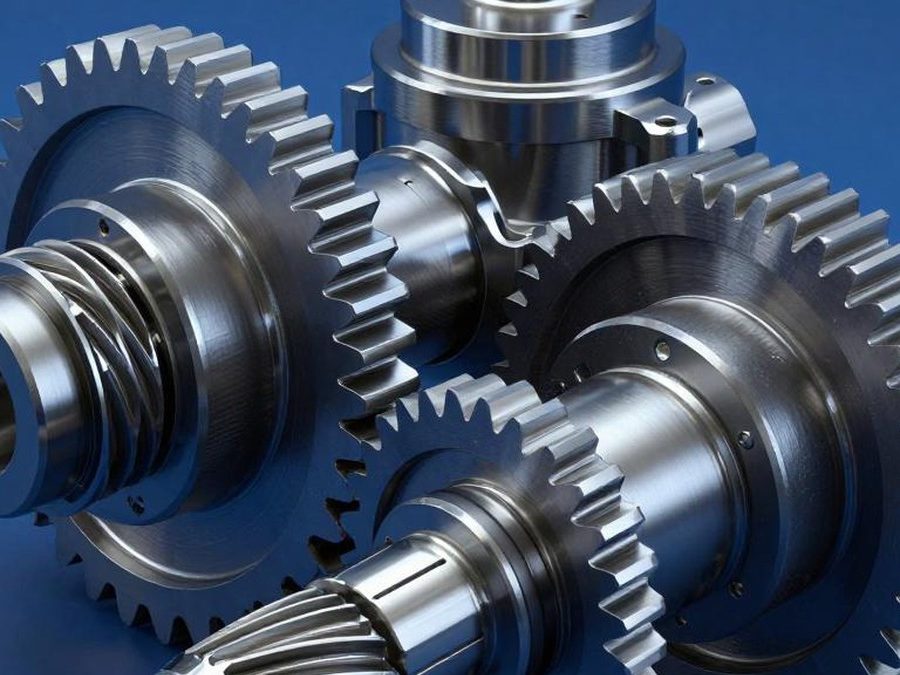
Gears are hobbed, shaped and profile-ground in house, then inspected for profile, lead and pitch deviation.
Heat treatment and surface hardness are controlled batch by batch so that meshing performance stays repeatable.
Key Features
- Module 0.5-8, up to 400 mm outside diameter
- Profile grinding to DIN 7 grade accuracy
- Carburizing and nitriding heat treatment in house
- Hardness 58-62 HRC after hardening
- Gear inspection report for profile, lead and pitch
- Matched sets and assembly service available